
OCTANE Products
OCTANE supplies precision-engineered products to the oil & gas, petrochemical, power generation, and water infrastructure sectors. Every product is sourced from approved manufacturers, fully traceable, and backed by our technical team.
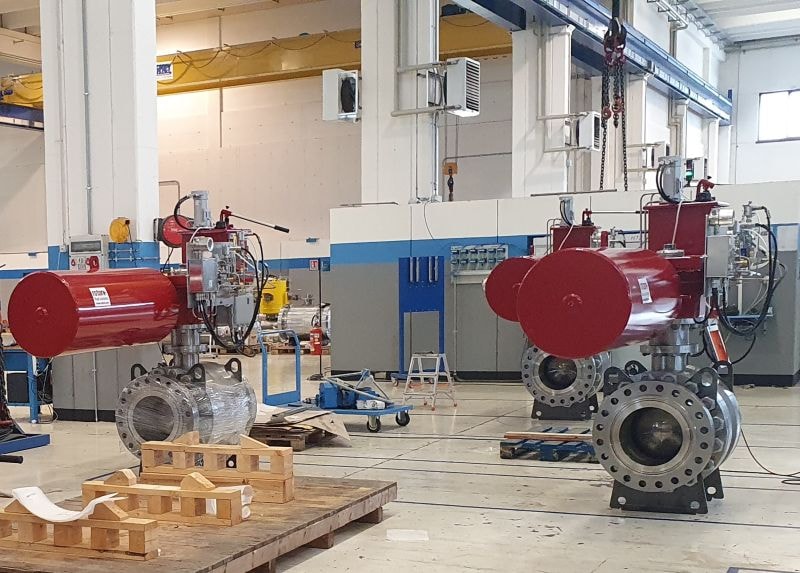
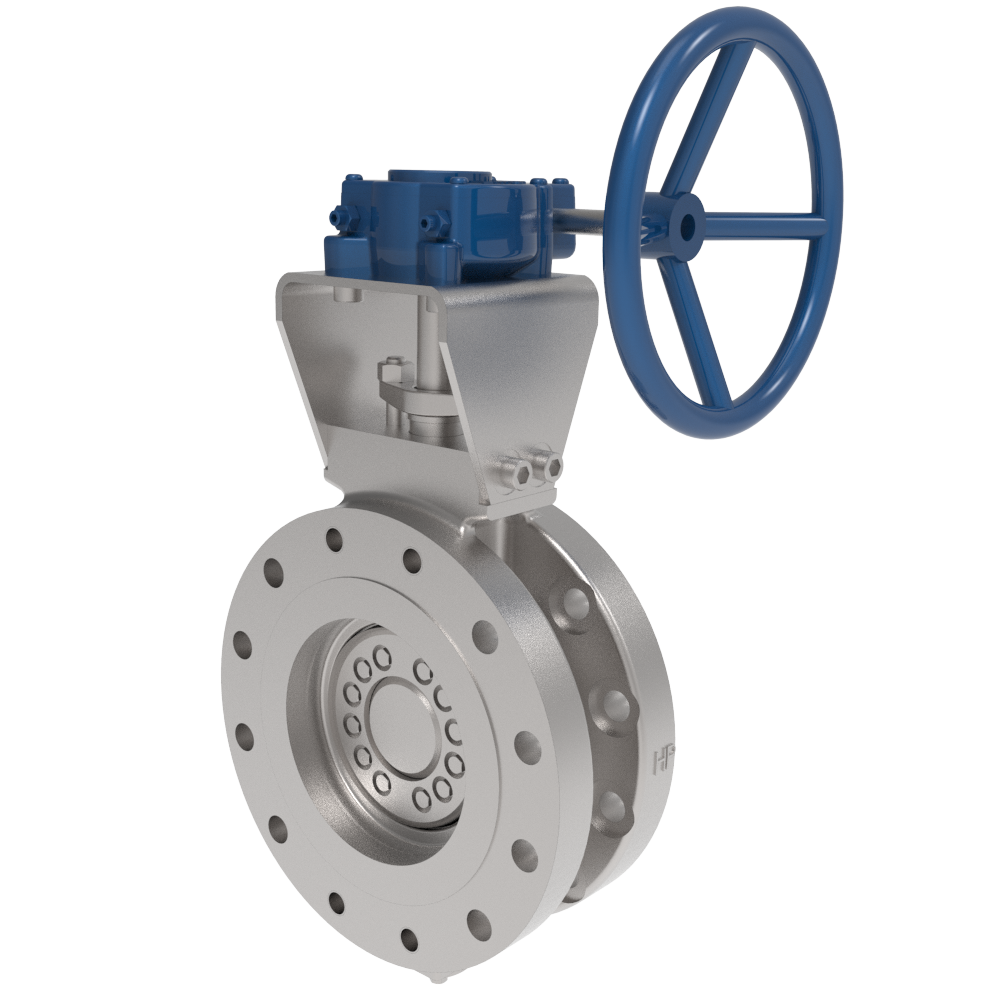
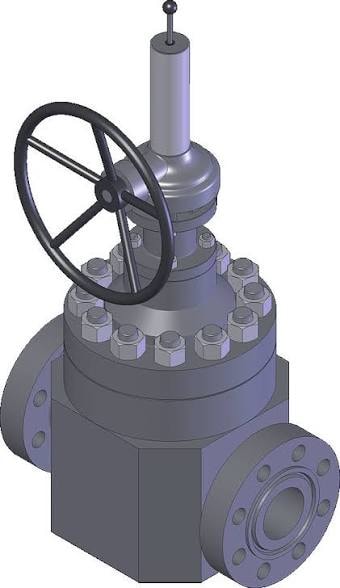
Valves
Precision-engineered valves for the most demanding process conditions.
OCTANE supplies a comprehensive range of industrial valves for oil & gas, petrochemical, power generation, and water treatment applications. Our valve portfolio covers every service condition: from cryogenic LNG and subsea to high-temperature, high-pressure wellhead and safety-critical isolation. All products are fully traceable and certified to international standards including API, ASME, and ISO.
11 Valve Categories — Full Portfolio
Ball Valves
Quarter-turn trunnion-mounted and floating ball valves for onshore, offshore, pipeline, cryogenic LNG, subsea, and hydrogen service. Certified to API 6D, API 6DSS, and ISO 14313, including HIPPS and high-integrity actuated packages.
Gate Valves
Cast and forged gate valves in rising and non-rising stem configurations to API 600 and API 602, including compact expanding gate and double disc parallel slide designs to API 6D / API 600.
Globe Valves
Multi-turn globe valves in straight, angle, Y-pattern, and bellows seal configurations for precise throttling and flow regulation, to BS 1873 / API 623 and ASME B16.34.
Check Valves
Non-return valves preventing reverse flow — swing check to API 594 / BS 1868, dual plate check to API 594, and axial check valves to API 6D.
Axial Valves
High-performance in-line axial check valves for minimal pressure drop and fast response to API 6D — ideal for compressor anti-surge, pipeline ESD, and high-cycle applications.
Butterfly Valves
Quarter-turn TOV butterfly valves for large-diameter, low-to-medium pressure service to API 609 in wafer, lug, and double-flanged configurations.
Pressure Safety Valves
Spring-loaded direct-acting safety relief valves for gas, vapor, and liquid service — ASME Section XIII "UV" stamped, National Board Certified, with 100% hydrogen compatibility.
Pressure Relief Valves
Pilot-operated relief valves for snap-acting and modulating service in ambient and cryogenic applications — ASME "UV" stamped, with set pressures from 10" wc to 15,000 psig.
Surge Relief Valves
Pilot-less modulating liquid surge relief valves protecting product pipelines from hydraulic surge and water hammer — 100 to 3,705 psig operating range.
Wellhead & Christmas Tree Valves
API 6A wellhead and Christmas tree valves for upstream production service, including rising stem ball valves (RSBV) for high-integrity isolation.
Rising Stem Ball Valves (RSBV)
Orion RSBV — cast or forged steel body, outside screw & yoke, rising stem, non-rising operator, renewable seats, removable yoke sleeve, and backseat for repacking under pressure. Torque-seated ball design ensures high tightness independently of differential pressure. No stem rotation during travel — minimising material wear and fugitive emissions. Available in ASME Class 150 through 2500 (PN 20–PN 250) in carbon steel, stainless steel, and CRA alloys.
Pressure Seal Valves
High-pressure / high-temperature gate and globe valves with pressure seal bonnet construction to ASME standards for critical process and power generation service.
Need a Specific Valve?
Our team can source, specify, and inspect any valve type for your application — including bespoke and hard-to-source items.

Field Instruments
Accurate, reliable instrumentation for critical process measurement.
From pressure transmitters and flow meters to temperature sensors and level gauges, OCTANE supplies field instrumentation from leading global manufacturers. Our instrumentation team works closely with clients to specify the right technology for each application, ensuring compatibility with existing control systems and compliance with hazardous area classifications.
- Pressure transmitters & gauges
- Flow meters — Coriolis, magnetic, ultrasonic, vortex
- Temperature sensors & transmitters
- Level gauges, switches & radar transmitters
- Analytical instruments & gas detectors
- HART, Foundation Fieldbus & Profibus compatible
- ATEX / IECEx hazardous area certified
- SIL-rated instruments for safety systems
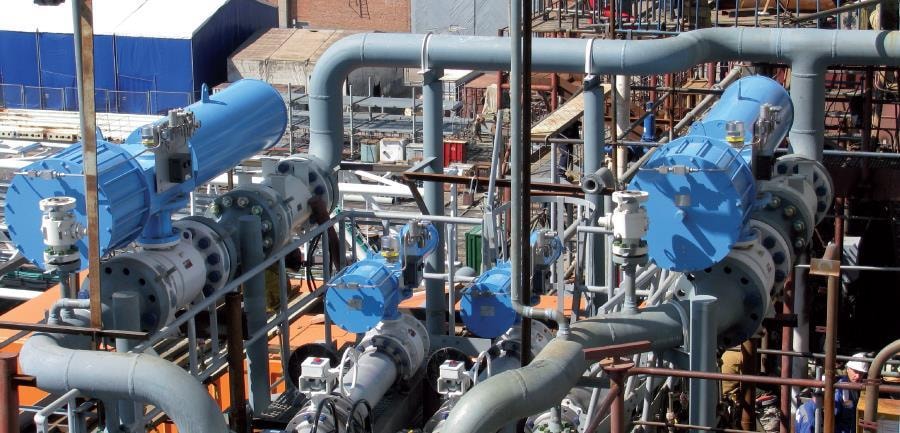
Actuators
Reliable actuation solutions for automated valve control in any environment.
OCTANE provides pneumatic and hydraulic actuators for valve automation across upstream, midstream, and downstream applications. Our actuation packages are engineered for standard and custom configurations — including fail-safe ESD service — with full control systems, hydraulic power units, and emergency accumulators. Certified to ISO 9001, ATEX, IECEx, SIL 3, PED, and NACE MR0175.
- Pneumatic quarter-turn actuators — for ball, butterfly, plug and rotary valves
- Pneumatic linear actuators — for gate, globe and linear control valves, on-off and modulating
- Hydraulic quarter-turn actuators — heavy duty, for ball, butterfly and plug valves
- Hydraulic linear actuators — for gate, globe and linear control valves, on-off and modulating
- Electro Hydraulic Self-Contained Actuators — integrated electric-driven hydraulic power unit in a single compact package
- Gas Over Oil Actuators — utilising line gas pressure to drive hydraulic fluid for remote and subsea applications
- Full Stainless Steel Actuators — for highly corrosive, offshore, and marine environments requiring full SS316 construction
- Special products — custom engineered actuators for critical and severe service
- Full control systems — complete units with pneumatic, hydraulic and electric equipment
- Hydraulic power units (HPU) & emergency accumulators
- Fail-safe circuits for emergency shutdown (ESD) service

Water & Utility
Engineered products for water treatment, desalination, pipeline integrity, and utility infrastructure.
OCTANE supports water treatment plants, desalination facilities, and industrial utility systems with a full range of engineered products — from chemical dosing systems and filtration equipment to pumps, heat exchangers, and process vessels. Our portfolio also includes a comprehensive range of pipe joining, repair, and tapping solutions for natural gas distribution, water/wastewater management, and industrial pipeline applications.
- Chemical dosing & injection systems
- Filtration & separation equipment
- Pumps — centrifugal, positive displacement, submersible
- Heat exchangers & pressure vessels
- Desalination plant components
- Pipe fittings, flanges & gaskets
- Water quality analysers & monitoring systems
- Utility skid packages & modular systems
- — Pipe Joining & Repair —
- Wide range pipe couplings — for nearly any diameter or pressure rating
- Large diameter pipe couplings — for transmission and distribution mains
- Leak encapsulation products — mechanical clamps and weldable sleeves for live pipeline repair
- Tapping & line stopping sleeves — for hot-tap connections without service interruption
- Dismantling & expansion joints — for flexible pipeline connections and maintenance access
- Flexible couplings — for misalignment, vibration isolation, and pipe movement compensation
- Emergency repair kits — rapid-response solutions for pipeline failures in the field
Need a Product
Specification?
Our technical team can help you select the right product for your application, prepare datasheets, and manage the full procurement and inspection process.